C012
ISO
SH725
50 - 200
0.01 - 0.05
SH725
50 - 200
0.01 - 0.05
SH725
50 - 200
0.01 - 0.05
SH725
50 - 200
0.01 - 0.05
SH725
150 - 200
0.01 - 0.05
SH725
100 - 200
0.01 - 0.05
SH725
30 - 80
0.01 - 0.05
SH725
30 - 80
0.01 - 0.05
STANDARD CUTTING CONDITIONS
HOW TO SELECT TOOLS
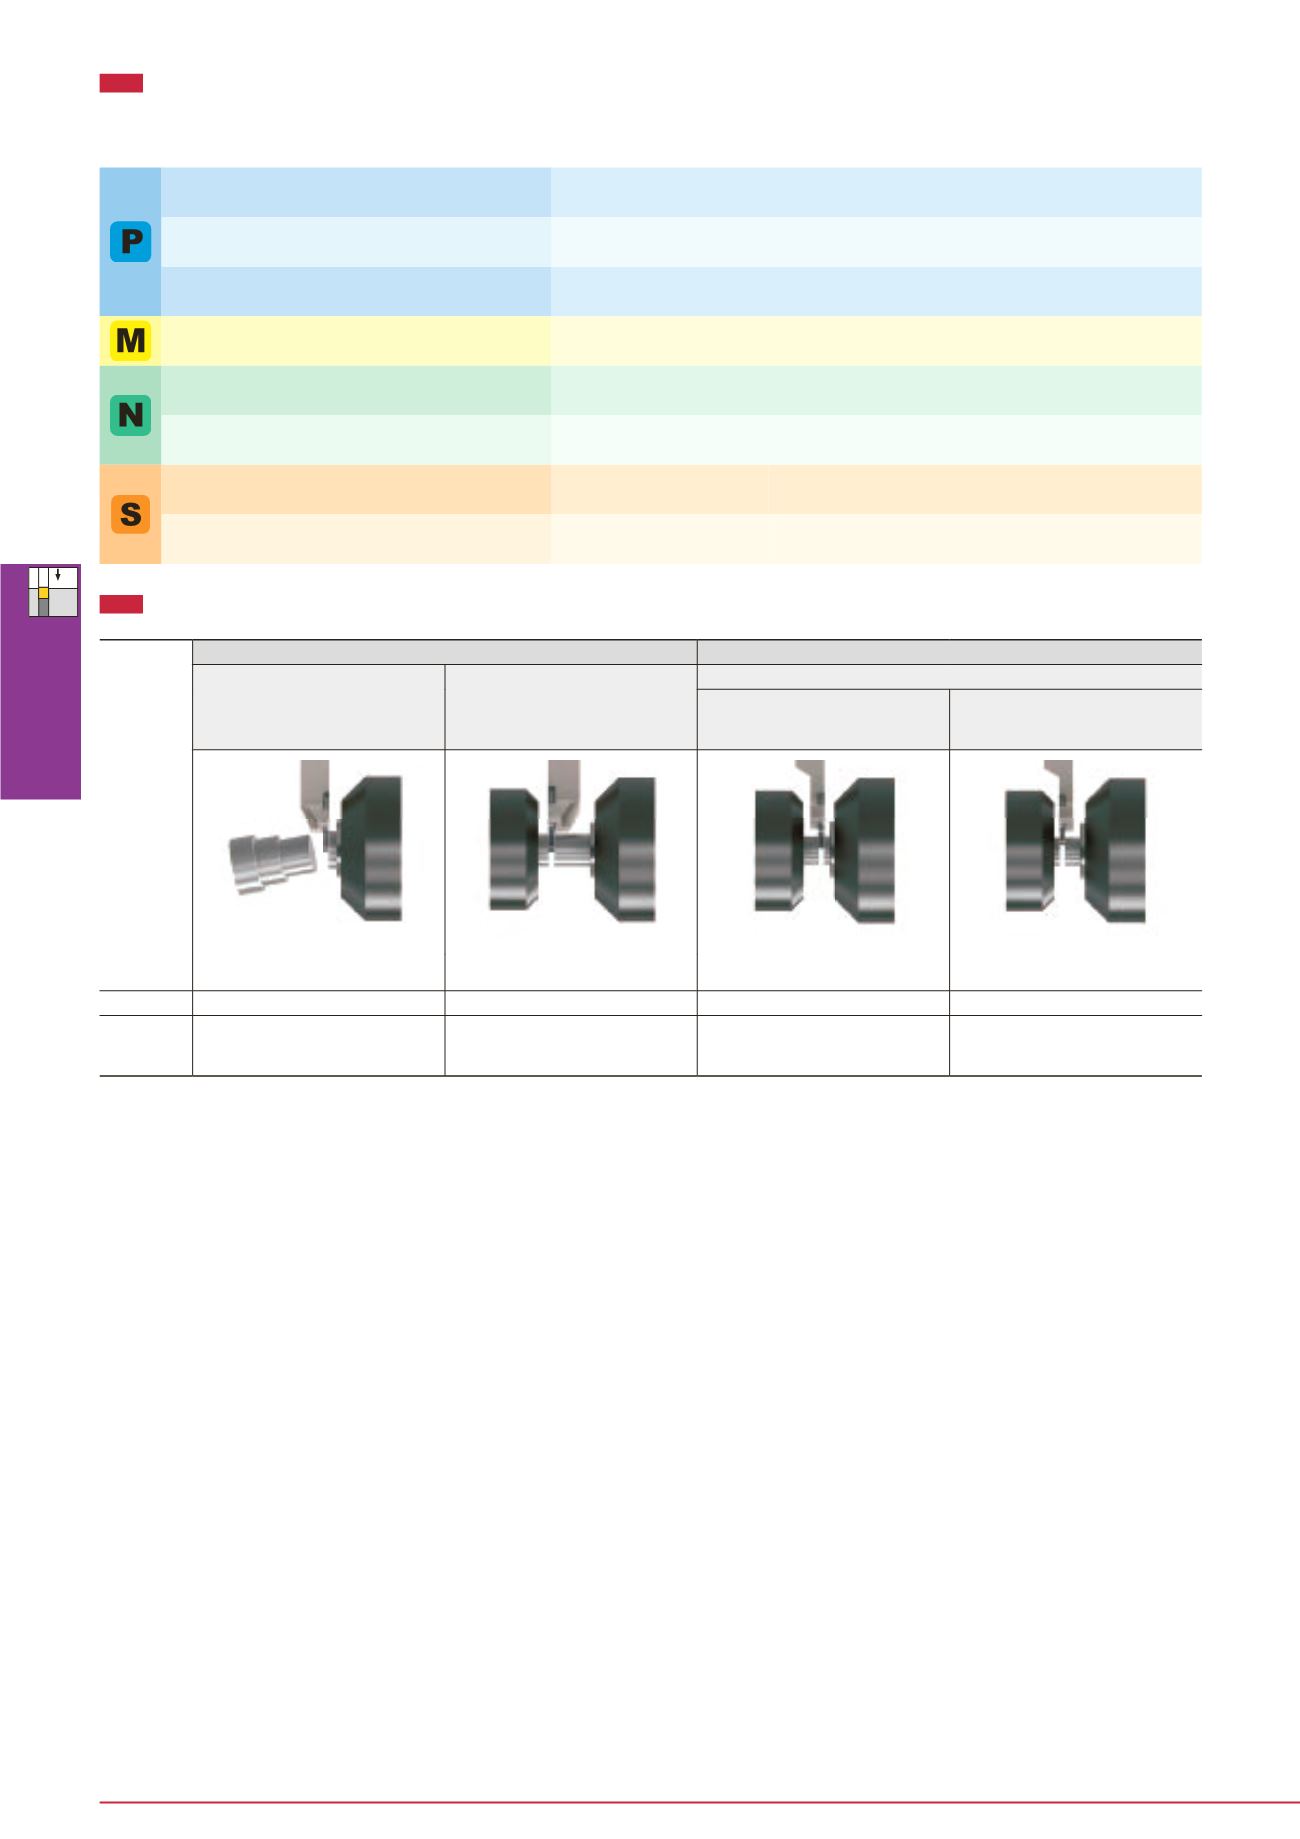
Large-diameter machining of workpiece with rigitity Small-diameter machining of workpiece with short overhang
Main-spindle tooling
Sub-spindle tooling
Sub-spindle tooling
Workpiece with long overhang
at the side of sub-spindle for
the process after parting-off
Short workpiece
with low rigitity
Position of parting-off is at the side
of the main spindle
Position of parting-off is at the side
of the sub-spindle
Position of parting-off is at the side
of the main spindle
Position of parting-off is at the side
of the sub-spindle
R-hand (JSXXR type)
L-hand (JSXXL type)
R-hand (JSXXR-S type)
L-hand (JSXXL-S type)
Right-hand insert with lead
angle to remove center core
(JXPG**R***-15 type)
Left-hand insert
(JXPG**L*** type)
Right-hand insert
(JXPG**R*** type)
Left-hand insert
(JXPG**L*** type)
Cutting speed
Vc (m/min)
Feed
f (mm/rev)
Workpiece material
Grade
Low carbon steels
C15, C20, etc.
Carbon steels, Alloy steels
C55, 42CrMoS4, etc.
Stainless steels
X5CrNi18-9, X5CrNiMo17-12-2, etc.
Titanium alloys
Ti-6AI-4V, etc.
Superalloys
Inconel718, etc.
Free cutting steels
X50CrSi8 2, etc.
Aluminium alloys
Copper alloy
Insert
Application
Toolholder
Main spindle
Main spindle
Main spindle
Main spindle
Sub-spindle
Sub-spindle
Sub-spindle
Grooving Tool


