Tungaloy
B175
DX110
DX120
DX140
DX160
DX180
< 1
5
13
28
45
DX120
0.05
0.04
0.03
0.02
0.01
0
DX140 DX160
0.2
0.1
0 3
6
12
DX140
DX160
DX180
DX120
DX110
DX140
12000
8500
ISO
DX110 DX120 DX140 DX160 DX180
1000 - 2500
0.05 - 2.0
0.05 - 0.2
400 - 800
0.05 - 2.0
0.05 - 0.2
500 - 1500
0.05 - 2.0
0.05 - 0.2
300 - 500
0.05 - 2.0
0.05 - 0.2
300 - 500
0.05 - 2.0
0.05 - 0.2
500 - 1000
0.05 - 0.5
0.03 - 0.1
500 - 1000
0.05 - 0.5
0.01 - 0.05
10 - 20
0.05 - 0.2
0.01 - 0.05
100 - 150
0.05 - 2.0
0.03 - 0.1
Insert
PCD / CBN
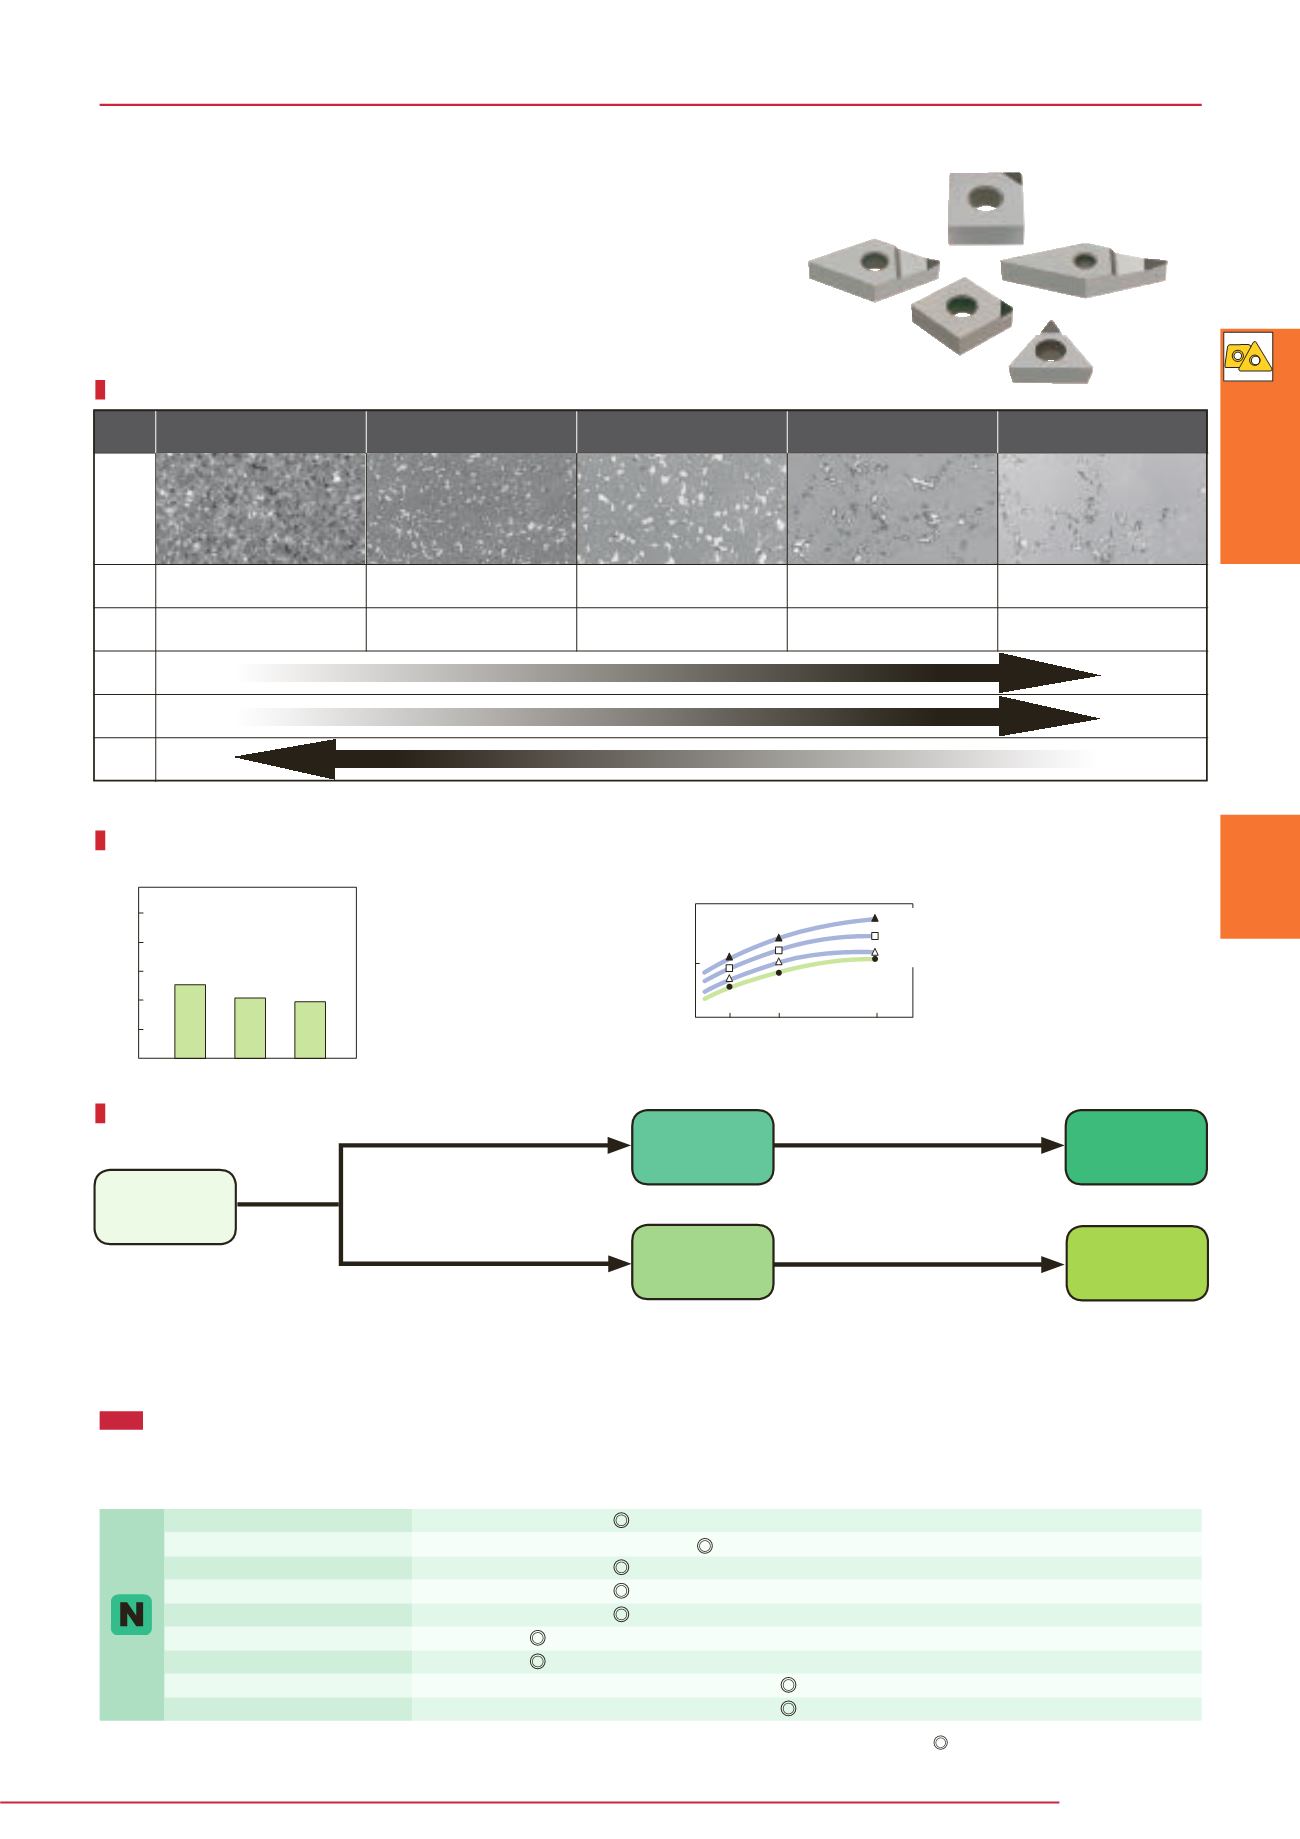
Expanded product line allows T-DIA tools to be
applied to wider workpiece materials and cutting
conditions.
Continuous external turning
Workpiece material:
10 % Si, aluminium alloy
Insert: SPGN120308-DIA
Toolholder: CSBPR2525M4
Cutting speed:
v
c
= 500 m/min
Feed:
f
= 0.1 mm/rev
Depth of cut:
a
p
= 0.5 mm
Coolant: Dry cutting
Time in cut: 30 min
When machining aluminium alloy:
Face milling
Workpiece material:
Fiber reinforced plastics (FRP)
Insert: SPCN42ZFR-DIA
Milling cutter: TPG4208R-A
Cutting speed:
v
c
= 942 m/min
Feed:
f
= 0.1 mm/rev
Depth of cut:
a
p
= 1.5 mm
Coolant: Dry cutting
When machining FRP:
Flank wear width:
V
B
(mm)
Flank wear width: V
B
(mm)
Time in cut (min)
CompetitorA
CompetitorB
CompetitorC
Cutting performance (Wear resistance)
Grade selection guide
Basic selection
(General purpose grade)
Excels in cutting-edge
sharpness and impact
resistance.
Super fine grained
grade
Special purpose
grade
Superior wear
resistance
For precision machining
When good surface finish is
required.
When interrupted cutting is
involved.
When machining hard materials
such as high silicon aluminium
alloys (Si > 12 %)
Simultaneous machining of
aluminium alloy and Cast iron.
When high wear resistance is required.
When requiring higher wear
resistance than DX160 (such
as when machining high
silicon materials, cemented
carbides, semi-sintered
ceramics, etc.)
Workpiece material
Cutting speed
v
c
(m/min)
Feed
f
(mm/rev)
Depth of cut
a
p (mm)
Grade applicability
Aluminium alloys (Si < 12 %)
Aluminium alloys (Si > 12 %)
Copper, brass
Phosphor bronze
Carbon, graphite
FRP
Plastics
Cemented carbides (D40 ~ D60)
Semi-sintered ceramics
(Note) : First choice
: Second choice
Features and applications (Physical and mechanical properties)
Higher
(Harder)
Super fine grained grade.
Excels in surface finish.
Fine grained grade.
Excels in surface finish.
General purpose grade
High purity grade for
hard materials
Highly wear resistant grade
for special applications
Grade
Property
Approx.
grain size
of diamond
(µm)
Hardness
(Hv)
Wear
resistance
Grindability
(Cutting
edge
sharpness)
Better
Note: T-DIA grades are not suitable for ferrous materials (such as hardened
steel
, chilled
Cast iron
), and Ni- or Co-base
Superalloys
.
STANDARD CUTTING CONDITIONS FOR TURNING
Turn
L i ne -
PCD grade, T-DIA ser ies


